
Temperature Sensor Overcomes Design Constraints in an Integrated Power Box
Challenge
The customer’s design engineers faced several constraints when placing a temperature sensing solution in their integrated junction power box. This design required two sensors placed in two different system locations. Functionally, the sensors would control a circuit that reduces current when an abnormal or fast temperature rise is detected.
The temperature sensor assemblies were intended to be mounted on busbars using lugs. However, the sharp edges of aluminum busbars can sometimes damage the wire insulation material of thermistor assemblies. This was especially problematic considering that the wire positions wouldn’t be fixed, as these systems often experience high mechanical shock and vibration forces during operation. Also, the busbars might be subjected to very high temperatures, which meant that standard plastic wire insulation alone wasn’t viable, as it could melt and cause a short.
As they would be employing two sensors of the same style in two different locations in the system — but with different R25 values and cable lengths — it was important to be able to distinguish between the two assemblies for selection and placement during manufacturing. The final solution also had to be compliant with AEC-Q200, offer a high isolation voltage of 2.7 kVAC up to +150 °C, and feature an M4 mounting screw size.
Solution
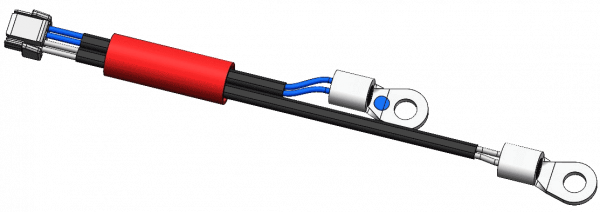
Vishay’s design engineers created an assembly based on the NTCALUG91A standard lug sensors, which feature an M4 screw mounting.
The final end product features two sensors with different cable lengths and wire colors mounted on the same connector. To protect the connection cables from the sharp edges on the busbars, they are in glass fiber insulation tubes. This wire casing masked the wire insulation colors and prevented visual inspection, which meant that another solution for differentiating the two sensors was necessary. It was decided to add a colored dot on the neck of the lug for one of the two sensors, which can be easily detected via automated visual inspection.
Benefit
This cost-effective solution offers our customer precise and secure temperature control of their integrated power box, prevents damage to the sensors and connecting cables, allows for variable design positions, and improves the reliability of the final application.
Additional Case Studies
Avoiding a Complete Redesign After a Panel Potentiometer was Made Obsolete
Challenge
The customer approached Vishay when their existing panel potentiometer supplier discontinued production of a part used on an established and popular piece of equipment. To avoid a costly redesign, an existing panel potentiometer needed to be adapted to meet the customer’s electrical requirements. It would also have to fit the control panel insertion / retention envelope and existing markings, in addition to the PCB assembly attachment system.

DC-Link Capacitors With Tab Terminals For Harsh Vibration Profiles
Challenge
Our customer was evaluating a solution for power electronics equipment that required the use of several DC-Link capacitors on the same PCB, while ensuring that the devices would support critical vibration profiles. The products being considered for the application had a significantly high mass of around 100 g, and were attached to the PCB via four lead wires with 1.2 mm diameters. While testing these parts under severe vibration profiles, the customer reported broken lead wires. The challenge was clear: how can such high mass parts withstand severe vibration profiles, while maintaining a similar footprint on the PCB?
mmWave Loss and Unstable Performance in a Satellite Payload
Challenge
While developing a next‑generation Ka‑band and W‑band satellite payload for a low‑Earth‑orbit communications constellation, an RF systems engineer encountered an unexpected challenge. Although the team designed a GaN power amplifier and low‑noise receiver chain to operate above 80 GHz, system testing revealed significant performance degradation. The active devices met their specifications, but once the signal left the die, system performance collapsed: Insertion loss exceeded the link budget by 1.5 dB Parasitic inductance from wire bonds and interconnects distorted matching Board-to-board variation caused gain and phase inconsistencies across flight units Commercial passive components were too large and introduced resonances above 70 GHz The design relied on an advanced organic PCB with thick‑film passives and LTCC modules. Despite extensive tuning and redesign cycles, performance drifted from build to build, introducing unacceptable risk to schedule and qualification.
Have questions? We can help.
This is our general contact form. If you have more specific questions or needs please select from the options below.